Light in Machine Vision
How to find the right lighting
Lighting in a vision system is often overlooked during the planning phase. Yet it is crucial for image quality and efficiency. Without the right light source, reflections and underexposed or overexposed areas can occur. Learn which light source is best suited for your system and what to look for when making your selection.
Last updated: 05/09/2023
Reading time: approx. 10 Minutes
Lighting techniques for Machine Vision
Different lighting techniques create distinct image representations of an object, highlighting different surface features and characteristics. Therefore, different lighting techniques can be used to address various inspection tasks.
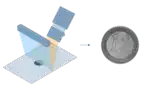
Headlight illumination
The camera and the light source are located on the same side relative to the object being viewed, so that the light is reflected off the 'objects surface. This technique is particularly ideal for matte, low-reflectivity surfaces. For highly reflective surfaces, additional diffuser films or specially designed diffusing lighting types are used.
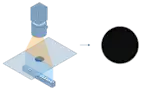
Transmitted light illumination
The object is positioned between the camera and the light source, with the light source located opposite the camera. Light passes through the object, causing it to partially or completely block the light entering the camera. As a result, only the outline is visible—for example, to precisely determine dimensions, object outlines, recesses, or fill levels for inspection and measurement tasks.
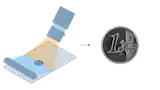
Dark field light
The light is directed onto the object at a shallow angle so that only areas lying at a specific angle to the camera reflect light. As a result, most of the image remains dark, while edges, scratches, engravings, and other surface defects become clearly visible due to bright reflections. This technique significantly increases the contrast and visibility of defects.
Types of lighting in machine vision
Choosing the right lighting is decisive to the effectiveness of an inspection task: Different lights are used to detect cracks than to distinguish colors. LED lights are the most commonly used in industrial image processing. These are cheaper and more efficient than, for example, halogen lamps or fluorescent tubes.
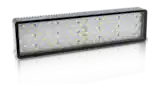
Bar light
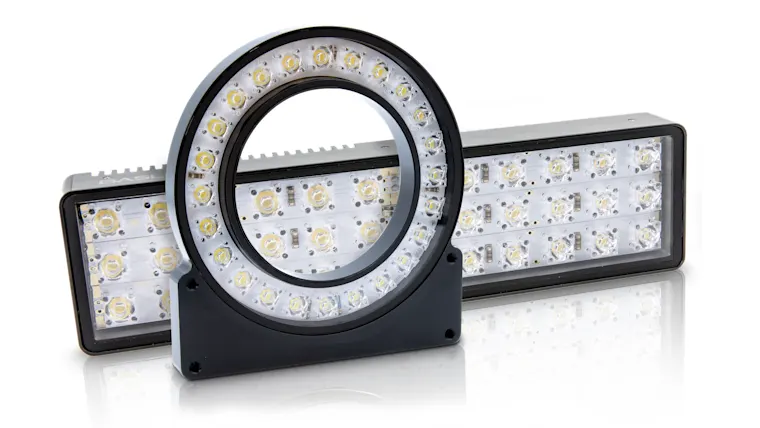
The light comes from an elongated bar and illuminates the object evenly. It is optimizedfor nearly all inspection tasks, such as inspecting long workpieces and highlighting object edges. In addition, bar lights can be used to illuminate only specific parts of an object. It is possible to combine multiple bar lights so that the object is illuminated from different sides. Since bar lighting can be aligned at a flexible angle to the object, it can also be used in darkfield applications.
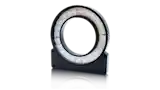
Ring light
A ring light is arranged in a circle around the lens, providing uniform, virtually shadow-free illumination of the test object. Due to its versatility, it is a standard lighting option in industrial image processing. Ring lights are frequently used in assembly monitoring, quality control, and optical inspection applications, as they enable homogeneous illumination of a wide variety of component geometries. For the targeted highlighting of surface structures, scratches, or other defects, darkfield illumination or other lighting techniques are often more efficient.
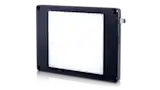
Back light
In this lighting technique, the object is evenly illuminated from behind to emphasize feature outlines or to screen an object. However, all information on the surface texture is lost. For example, holes, bubbles, or scratches can be identified and highlighted. Back light is also an important standard in the quality control of labels and printed paper.
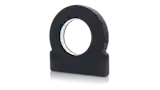
Horizontal ring lighting
With this type of lighting, unlike with standard ring lighting, the object is illuminated from the side rather than directly from the front. This causes light to be reflected into the camera, particularly along the edges. This ensures that contrasts are clearly defined and scratches are easily visible. Darkfield illumination is particularly important for transparent objects, such aswindows or films, as the lateral light source prevents shadows or reflections from forming.
Lighting brightness
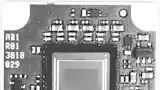
The brightness of the lighting is crucial for reliable image capture: Too little light results in noisy or dark images. Too much light can overexpose details and cause information to be lost. Optimal brightness ensures high contrast and uniform illumination of the object being inspected. It forms the basis for stable and reproducible measurement results in vision systems.
Not enough light
Insufficient light results in dark, noisy images, making it difficult to detect fine details. Contours and structures become blurred or are lost entirely. Image analysis becomes unreliable, and errors in inspection increase.
Too much light
Too much light leads to overexposure. This can cause important details and information to be lost. Bright areas appear flat, and reflections can further impair image quality. The risk of misinterpretation increases.
Using light in machine vision specifically for quality assurance
In image processing, you can take advantage of even more properties of light. Depending on the wavelength and material, light is refracted, absorbed, transmitted, or reflected. Choosing the right wavelength—or light color—plays a key role in achieving optimal image results.
Targeted contrasts through colored light
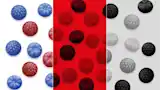
The color of light determines how surfaces appear, as it controls contrast. Complementary colors appear darker, while similar colors appear brighter. White light is suitable for natural color reproduction with color cameras, while blue or red light can be used with monochrome cameras to highlight or hide details.
Invisible wavelengths: IR light
Light is visible to the human eye in the range of 400 nm to 700 nm, with each wavelength corresponding to a different perceived color. Light beyond this visible spectrum can reveal features that are otherwise invisible to humans: For example, pressure marks on fruit can be detected particularly well with infrared (IR) light using SWIR cameras and illumination techniques. SWIR illumination
Invisible wavelengths: UV light
Ultraviolet (UV) light, with wavelengths below 400 nm, reveals hidden details through fluorescence or changes in reflectivity—such as security features, adhesive residue, or hairline cracks—using UV cameras and illumination techniques. UV Illumination such structures can be identified efficiently and reliably.
Targeted light manipulation
Through targeted manipulation of light, surface structures can be made visible, reflections can be controlled, and contrasts can be enhanced. With appropriate lighting strategies, the light is precisely tailored to the inspection task, thereby increasing process reliability and reproducibility in quality assurance.
Diffuse lighting
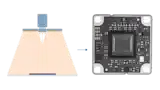
Diffuse lighting distributes light evenly across the object being inspected, thereby minimizing distracting shadows and reflections. This makes details visible—especially on shiny, textured, or uneven surfaces—that are often lost with directional lighting. Typical applications include the inspection of plastic parts, printed circuit boards, or metallic surfaces. Diffusers, light domes, or special panel lights are used to achieve this effect.
Polarized lighting
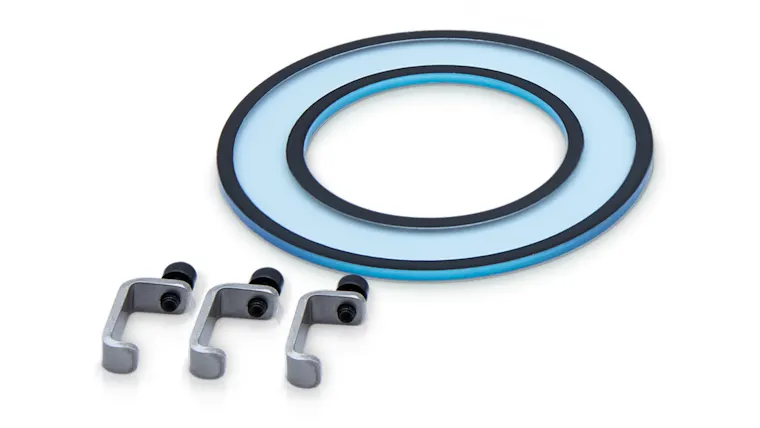
Polarized lighting specifically reduces or highlights unwanted reflections by using polarization filters on both the light source and the camera. This significantly minimizes reflections on non-metallic surfaces such as glass, plastic, or painted surfaces (the effect is often limited on metallic surfaces). This improves the detection of scratches, cracks, or other surface defects and increases image contrast for reliable evaluation.
Coordinating your lighting
Lighting is only one part of the vision system. However, the choice of lighting technology is decisive for the image quality: The quality of the light source cannot be balanced by other components. Therefore, when putting together your vision system, you should deal extensively with the topic of lighting.
How to choose your lighting
First, you narrow down the object characteristics that you want to make visible. Furthermore, various properties of the object under consideration are important. What material is it made of? Reflects or absorbs as well as the given lighting conditions and the distance to the object influence the choice of lighting.
Based on these factors, you can accurately determine which lighting is right for your project. For additional support, our Illumination Selector gives you individual product recommendations. It guides you step-by-step to a selection of coordinated lighting.
Our lighting products
Choose the right product for your vision system from our broad portfolio.
Frequently asked questions about proper lighting
White light is used when the goal is to achieve the most natural color reproduction possible. Colored light—such as blue, red, or infrared—is typically used with monochrome cameras to make specific features more visible through differences in contrast.
Infrared light can reveal features that are invisible to the human eye. This makes it particularly well-suited for workplaces where visible light would be a distraction.
Depending on the color of the light, certain colors on the test object appear lighter or darker. For example, blue light makes blue and white areas stand out, while red and green areas appear darker.
Lighting from many different angles—such as with a ring light—hides scratches and highlights other important features, such as imprints or colors, without casting distracting shadows.
When photographing highly reflective objects, diffuse light sources or additional diffuser sheets should be used to minimize distracting reflections and achieve uniform illumination.